Reinforced Barbed Tape Wire Factory
Reinforced barbed tape wire combines high-tensile steel core with helically wound barbed tape to create a perimeter security barrier designed for demanding industrial environments. Unlike standard
Reinforced Barbed Tape Wire: Technical Specifications and Industrial Applications
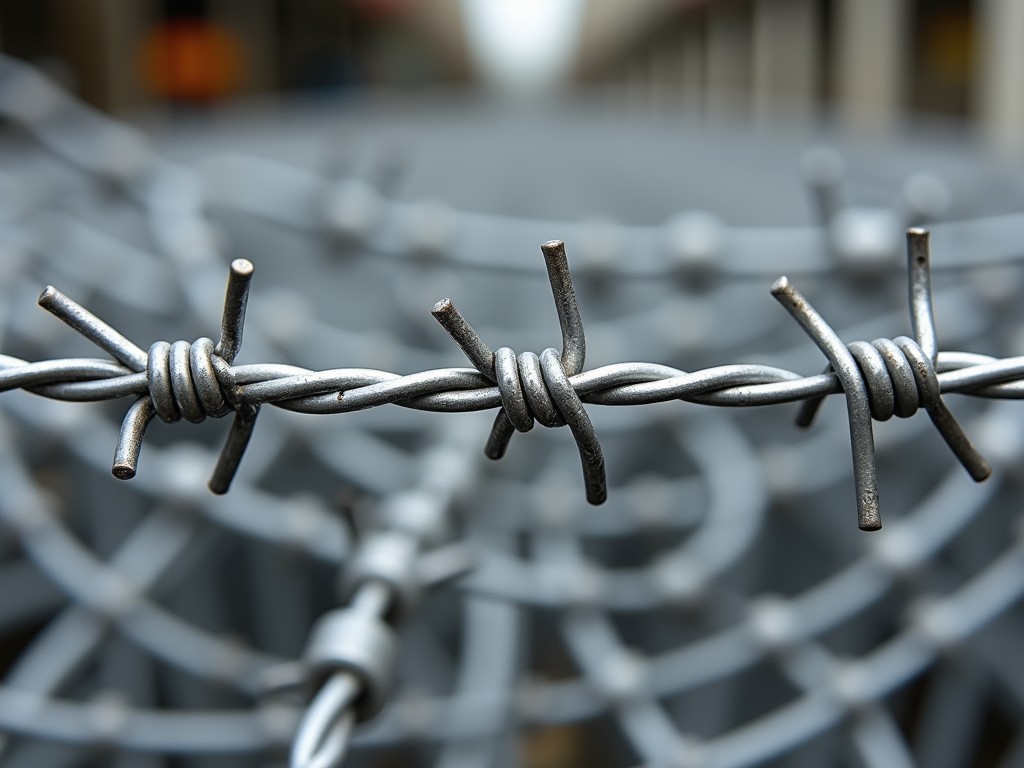
Reinforced barbed tape wire combines high-tensile steel core with helically wound barbed tape to create a perimeter security barrier designed for demanding industrial environments. Unlike standard barbed wire, the tape component increases surface area and cutting resistance while maintaining flexibility during installation. This hybrid construction addresses limitations of both conventional barbed wire (limited penetration resistance) and razor tape (brittleness under impact) by distributing load across the steel core while presenting multiple sharp edges to deter climbing or cutting attempts.
The reinforcement refers to the central steel wire, typically cold-drawn to achieve tensile strengths between 1,700–2,100 MPa, which prevents sagging over long spans and maintains barrier integrity under dynamic loads such as wind pressure or attempted breaches. The barbed tape, usually formed from 0.5–0.8 mm thick steel strip, is precision-rolled to produce uniform barbs with consistent geometry—critical for predictable performance in security applications. Manufacturing tolerances for barb height, spacing, and tape width directly influence the barrier’s effectiveness and are controlled within ±0.1 mm during production.
Industrial buyers evaluate reinforced barbed tape wire based on three interdependent factors: material selection for environmental durability, geometric consistency for reliable deterrence, and installation compatibility with existing infrastructure. The following sections detail these aspects to support informed specification decisions.
Material Composition and Corrosion Resistance
The steel core undergoes controlled cold drawing to achieve the required tensile strength while maintaining ductility for coiling and handling. Carbon content typically ranges from 0.60–0.80%, with manganese additions (0.30–0.60%) to enhance hardenability without compromising weldability if field repairs are necessary. Trace elements like silicon (0.10–0.30%) improve oxidation resistance during high-temperature processing. These compositional controls ensure the core resists permanent deformation under sustained tension—critical for barriers exceeding 100 meters in length between support posts.
The barbed tape is manufactured from low-carbon steel strip (C < 0.15%) to facilitate forming and ensure consistent barb geometry. To prevent premature corrosion, both components receive protective coatings applied via continuous hot-dip galvanizing or zinc-aluminum alloy plating. Coating thickness is measured in grams per square meter (g/m²), with standard industrial specifications requiring minimum 275 g/m² zinc (equivalent to ~40 μm) for moderate environments. For coastal or industrial zones with high chloride exposure, zinc-aluminum coatings (e.g., 55% Al-Zn) at 200 g/m² provide superior barrier protection due to aluminum’s passive oxide layer.
Coating adhesion is validated through bend testing—where coated wire is wrapped around a mandrel equal to its diameter without cracking or flaking—and salt spray resistance per ASTM B117. Typical performance exceeds 500 hours to red rust for hot-dip galvanized coatings in industrial atmospheres, though actual service life depends on localized factors like pH, pollution levels, and maintenance access. Buyers should specify coating weight and type based on environmental corrosivity categories (ISO 12944-2) rather than assuming generic “galvanized” suffices.
Barb Geometry and Security Performance
Barb effectiveness depends on three geometric parameters: height (distance from tape base to barb tip), throat width (opening at barb base), and blade angle (inclination relative to tape axis). Standard reinforced barbed tape wire features barbs 8–12 mm high with throat widths of 3–5 mm and blade angles between 25°–35°. These dimensions optimize penetration resistance while minimizing tape weakening—excessive barb height increases stress concentration at the root, raising fracture risk during impact or temperature cycling.
Barb spacing, typically 10–15 mm center-to-center, determines the frequency of deterrent points along the barrier. Closer spacing increases material cost and weight but improves coverage for applications requiring high climb deterrence, such as prison perimeters or military installations. Wider spacing reduces material usage but may create gaps exploitable by determined intruders using tools or body positioning. The optimal balance is determined through threat modeling—evaluating likely intrusion methods (bare hands, gloves, wire cutters) and required delay time for security response.
Unlike razor tape, which relies on sharp edges for laceration, reinforced barbed tape wire combines tensile strength with mechanical interlock: the barbs catch on clothing or equipment, creating resistance that must be overcome before cutting the core can be attempted. This dual-action mechanism increases effective delay time compared to single-function barriers. Performance is not quantified by standardized ratings but is assessed through simulated intrusion tests using standardized tools and protective gear, with results documented in manufacturer test reports available upon request.
Manufacturing Process and Quality Control
Production begins with drawing high-carbon steel wire to the specified core diameter (typically 2.5–3.0 mm), followed by cleaning and annealing to relieve drawing stresses before coating. The barbed tape is formed separately: steel strip is slit to width, edge-conditioned, then passed through rotating dies that stamp and bend the barb profile in a single continuous operation. Precision is critical—die wear or misalignment causes barb height variation, which creates weak points where intruders may focus cutting efforts.
After forming, the tape is helically wound around the core wire under controlled tension to ensure uniform pitch and prevent twisting or bunching. Winding tension affects final product stiffness: too loose allows lateral movement reducing barrier effectiveness; too tight induces residual stress that may cause premature fatigue. Automated tension monitoring with closed-loop control maintains consistency within ±5% of target value across production runs.
Quality control includes inline measurement of barb dimensions using laser gauges, coating thickness via X-ray fluorescence, and tensile strength of samples pulled from each batch. Finished product is inspected for visual defects (barb deformation, coating gaps, kinks) and dimensional compliance (diameter, barb pitch, tape width). Statistical process control (SPC) charts track key variables, with automatic alerts if measurements approach control limits. Final verification includes coiling tests—ensuring the product unwinds smoothly without tangling or barb damage—and packaging integrity checks.
Industrial Applications and Environmental Suitability
Reinforced barbed tape wire is selected where standard barbed wire lacks sufficient penetration resistance and razor tape is unsuitable due to brittleness or handling hazards. Common applications include securing substations against copper theft, perimeter protection for water treatment facilities, and buffer zones around data centers where visual deterrence must complement electronic surveillance. Unlike flexible mesh barriers, it provides immediate physical resistance without requiring tensioning systems or specialized posts—standard Y-stakes or angle iron posts spaced 3–5 meters apart are sufficient for most installations.
In transportation infrastructure, it secures railway yards and highway maintenance depots where ground vibration from passing traffic accelerates fatigue in less robust barriers. The steel core’s high tensile strength resists cyclic loading from wind-induced oscillation, while the tape’s flexibility accommodates minor ground settlement. For temporary installations—such as construction sites or event venues—the product can be reused if coating remains intact and barbs show no permanent deformation after removal, provided it was stored dry and coiled on appropriately sized drums to avoid kinking.
Environmental suitability depends on coating selection and installation practices. In acidic soils (pH < 5.5), zinc coatings may corrode rapidly; here, polymer-overcoated galvanizing or stainless steel cores (e.g., 304 grade) are recommended despite higher cost. In marine atmospheres, zinc-aluminum coatings outperform pure zinc due to sacrificial aluminum protection. Proper installation avoids direct contact with dissimilar metals (e.g., copper grounding rods) to prevent galvanic corrosion, using insulating sleeves or maintaining minimum 50 mm separation as specified in ISO 1461 guidelines.
Comparison with Alternative Perimeter Security Solutions
| Parameter | Standard Barbed Wire | Reinforced Barbed Tape Wire | Razor Tape |
|---|---|---|---|
| Core Tensile Strength (MPa) | 800–1,200 | 1,700–2,100 | 600–900 (tape only) |
| Barb/Tape Thickness (mm) | 1.6–2.0 (wire) | 0.5–0.8 (tape) | 0.5–0.8 (tape) |
| Impact Resistance | Low (wire bends easily) | High (core resists deformation) | Very Low (tape fractures) |
| Coiling Memory | High (requires stiff handling) | Moderate (balanced flexibility) | Low (prone to tangling) |
| Typical Coating Life (Years, Industrial) | 10–15 | 12–18 | 5–8 |
| Installation Complexity | Low | Low | High (requires gloves, special tools) |
Note: Values represent typical ranges for comparable products. Actual performance depends on specific material grades, coating types, and environmental conditions. Coating life estimates assume proper installation and minimal mechanical damage.
Customization Options and Ordering Considerations
Manufacturers offer adjustments to core diameter (2.0–3.5 mm), tape width (15–25 mm), barb height (6–15 mm), and spacing (8–20 mm) to match specific threat levels and installation constraints. Core material can be upgraded to galvanized high-tensile steel or stainless steel grades (304, 316) for corrosive environments, while tape may receive polymer coatings (e.g., PVC, polyethylene) in colors beyond standard galvanized gray—such as green for vegetation blending or black for low-visibility applications. These modifications affect weight, tensile strength, and coating adhesion, requiring requalification of performance characteristics.
Length per coil typically ranges from 50 to 200 meters, constrained by handling equipment and transportation logistics. Heavier gauges or wider tapes reduce maximum coil length to maintain manageable roll weight (usually under 25 kg for manual handling). End treatments include looped ends for easy tying or welded loops for permanent fixation, though the latter increases cost and complicates removal. Packaging options include water-resistant kraft paper with UV-resistant poly inner wrap or reusable plastic drums for corrosive environments, with labeling that includes batch number, coating specification, and production date for traceability.
Before quotation, suppliers require: intended application (to assess threat level), environmental conditions (ISO 12944 corrosivity category), post spacing and height, required coil length, and any regulatory standards (e.g., prison security, military specs). Providing this information enables accurate material recommendation and avoids over-specification—such as specifying stainless steel in dry inland areas where galvanized suffices—or under-specification that compromises security. Lead times vary from 2–4 weeks for standard configurations to 6–8 weeks for customized materials, depending on raw material availability and production scheduling.
For technical inquiries, custom specifications, or to discuss your perimeter security requirements, contact our engineering team.
Request Technical Consultation
More Products

Send Inquiry
If you are interested in our products, leave your information here and we will be in touch shortly.