Mig Welding Stainless Steel With Flux Core
Flux-cored arc welding (FCAW) with stainless steel wire is a specialized process used when the deposition rates and penetration characteristics of MIG welding are needed, but environmental conditions
MIG Welding Stainless Steel with Flux-Cored Wire: Technical Considerations
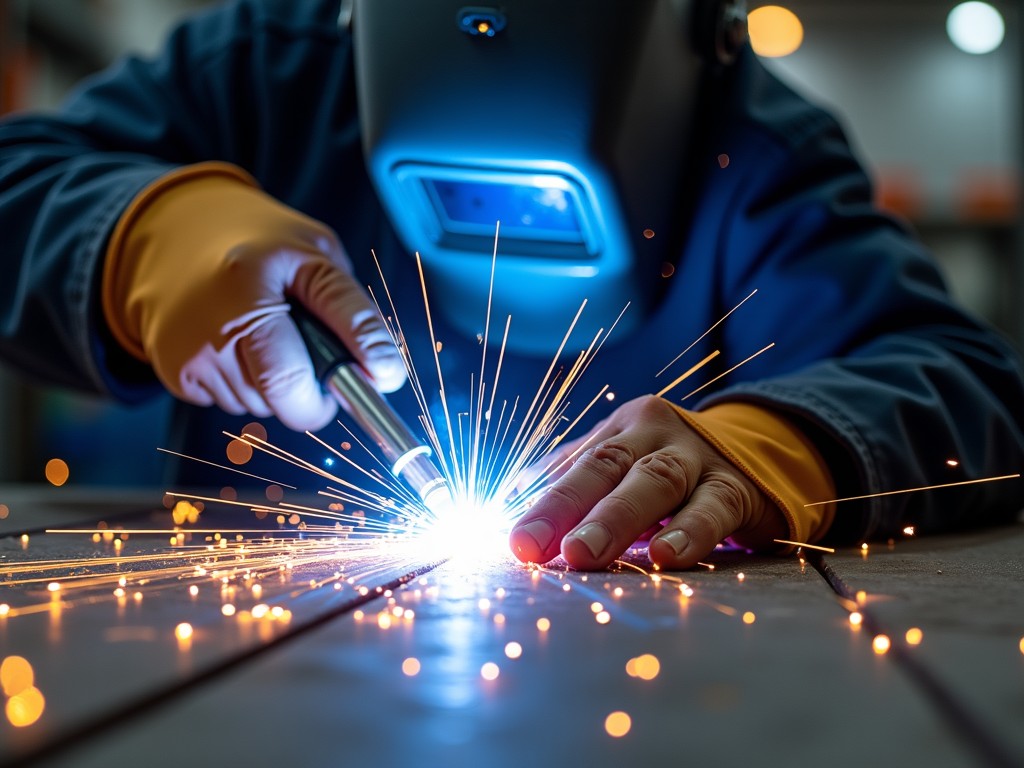
Flux-cored arc welding (FCAW) with stainless steel wire is a specialized process used when the deposition rates and penetration characteristics of MIG welding are needed, but environmental conditions or joint accessibility limit the use of solid wire and shielding gas. This method combines the efficiency of continuous wire feeding with the self-shielding or gas-shielded protection of a flux core, making it suitable for certain fabrication and repair scenarios involving stainless steel alloys.
The flux core in these wires contains deoxidizers, alloying elements, and slag formers that stabilize the arc, protect the weld pool from atmospheric contamination, and influence the chemical composition and mechanical properties of the deposited metal. When welding stainless steel, maintaining corrosion resistance and avoiding sensitization (chromium carbide precipitation) are critical, which requires careful selection of wire chemistry and control of heat input.
Wire Classification and Chemistry
Stainless steel flux-cored wires are classified under AWS A5.22 and typically designated as E308LT0-1/4, E309LT0-1/4, or E316LT0-1/4 for gas-shielded variants, where the "T" indicates tubular (flux-cored) construction, "0" denotes suitability for all positions, and the "-1/4" suffix refers to usability with direct current electrode positive (DCEP) and 100% CO2 or argon/CO2 mixes. Self-shielded variants (E308LT0-3/4, etc.) rely entirely on the flux core for protection and are less common for stainless steel due to challenges in achieving consistent corrosion resistance.
The "L" in the designation signifies low carbon content (max 0.04%), which minimizes the risk of sensitization during welding. For example, E308LT0-1/4 wire typically contains approximately 18-21% chromium, 9-11% nickel, and a controlled manganese level to promote weld pool fluidity without excessive spatter. The flux formulation includes silicates and fluorides to stabilize the arc and form a removable slag layer that protects the weld bead during cooling.
Shielding Gas Requirements
Gas-shielded flux-cored stainless steel wires require external shielding gas to achieve optimal weld quality, with argon-based mixtures being standard. The most common shielding gas is C2 (98% argon, 2% CO2) or a tri-mix of 90% helium, 7.5% argon, and 2.5% CO2 for improved penetration and bead appearance in out-of-position welding. Using 100% CO2 is possible but often results in higher spatter, a more convex bead profile, and potential reduction in corrosion resistance due to increased carbon pickup from the atmosphere.
Flow rates typically range from 20 to 25 CFM (cubic feet per minute), depending on wire diameter and joint configuration. Insufficient gas flow can lead to porosity and oxidation, while excessive flow may cause turbulence that draws in ambient air, particularly in drafty environments. Proper gas lens selection and torch-to-work distance (usually 1/2 to 3/4 inch) are essential for maintaining laminar gas coverage over the weld pool.
Parameter Settings and Technique
Welding parameters for flux-cored stainless steel wire are influenced by wire diameter, shielding gas, base metal thickness, and position. For 0.035-inch (0.9 mm) E308LT0-1/4 wire welding 1/4-inch austenitic stainless steel in the flat position with C2 gas, typical settings are 24-26 volts and 180-200 amps, yielding a deposition rate of approximately 4-5 lbs/hr. Increasing voltage widens the bead and reduces penetration, while decreasing voltage increases penetration but risks lack of fusion if too low.
Travel speed should be adjusted to maintain a slight lead angle (5-15 degrees) in the direction of travel, with the wire positioned at the leading edge of the weld pool. A push technique (dragging the wire away from the weld pool) is generally preferred for better gas coverage and cleaner bead appearance, whereas a drag technique may increase porosity risk. Interpass temperature should be monitored and kept below 350°F (177°C) for austenitic stainless steels to avoid overheating and potential loss of corrosion resistance in the heat-affected zone.
For out-of-position welding (vertical up, overhead), reducing amperage by 10-15% and using a shorter stick-out (3/8 inch) helps control the weld pool and prevent sagging. The flux core’s rapid solidification properties assist in supporting the molten metal, but excessive heat input can still cause collapse or undercut.
Advantages and Limitations Compared to Solid Wire MIG
The primary advantage of flux-cored stainless steel wire over solid wire MIG is higher deposition rates at comparable amperage, due to the higher current density achievable with tubular construction and the arc-stabilizing effects of the flux core. This makes FCAW particularly effective for filling large joints, building up wear-resistant overlays, or welding thick sections where productivity is a priority. The slag layer also provides visible protection during cooling, reducing the risk of atmospheric contamination in less-than-ideal shielding conditions.
However, flux-cored welding produces more slag that must be removed between passes, adding post-weld cleaning time. The wire is generally more expensive per pound than solid stainless steel wire, and the process generates higher levels of fumes due to the decomposition of flux compounds, requiring adequate ventilation or fume extraction. Additionally, achieving the same level of corrosion resistance as solid wire with proper shielding can be more challenging, particularly if welding parameters are not tightly controlled or if low-hydrogen practices are not followed.
Typical Applications
Flux-cored stainless steel welding is commonly used in the fabrication of food processing equipment, pharmaceutical machinery, and chemical storage tanks where joint accessibility favors high-deposition processes and post-weld cleaning is feasible. In shipbuilding and offshore structures, it is applied to weld stainless steel cladding on carbon steel substrates or to repair corrosion-resistant overlays where mobility and speed are essential. The process is also utilized in maintenance and repair operations involving stainless steel piping systems, where the ability to weld in windy outdoor conditions (with gas-shielded wire) or confined spaces (with self-shielded variants, though less preferred) offers operational flexibility.
It is generally not recommended for thin-gauge stainless steel (< 1/8 inch) due to the higher heat input and penetration characteristics, which increase the risk of burn-through or distortion. For aesthetic applications requiring minimal post-weld finishing, solid wire MIG with pulsed spray transfer is often preferred over flux-cored alternatives.
Quality Control and Post-Weld Considerations
After welding, the slag must be completely removed using a chipping hammer and wire brush to allow for proper visual inspection and to prevent crevice corrosion. Penetrant testing or magnetic particle inspection (for ferritic grades) may be conducted to detect surface-breaking defects. For critical corrosion-resistant applications, intergranular corrosion testing (e.g., ASTM A262 Practice E) can be performed to verify that sensitization has not occurred, particularly if the weld was exposed to temperatures between 800°F and 1500°F (427°C–815°C) for extended periods.
Ferrite content should be monitored when welding austenitic stainless steels to avoid hot cracking; a ferrite number between 3 and 10 is typically desired for welds made with E308L or E316L filler metals. This can be estimated using a WRC-1992 diagram based on the chemical composition of the weld deposit, which is influenced by both the wire chemistry and dilution from the base metal. Post-weld heat treatment is rarely required for austenitic stainless steels unless stress relief is needed to reduce distortion risk, in which case temperatures should not exceed 900°F (482°C) to avoid sensitization.
For technical consultation on selecting the appropriate flux-cored stainless steel wire for your welding application, including parameter optimization and joint design review, contact our engineering team.
Request Technical Support
More Products

Send Inquiry
If you are interested in our products, leave your information here and we will be in touch shortly.