Welding Stainless Steel With Regular Mig Wire
Industrial buyers evaluating welding processes for stainless steel components often question whether standard carbon steel MIG wire (such as ER70S-6) can be used effectively. This page explains the
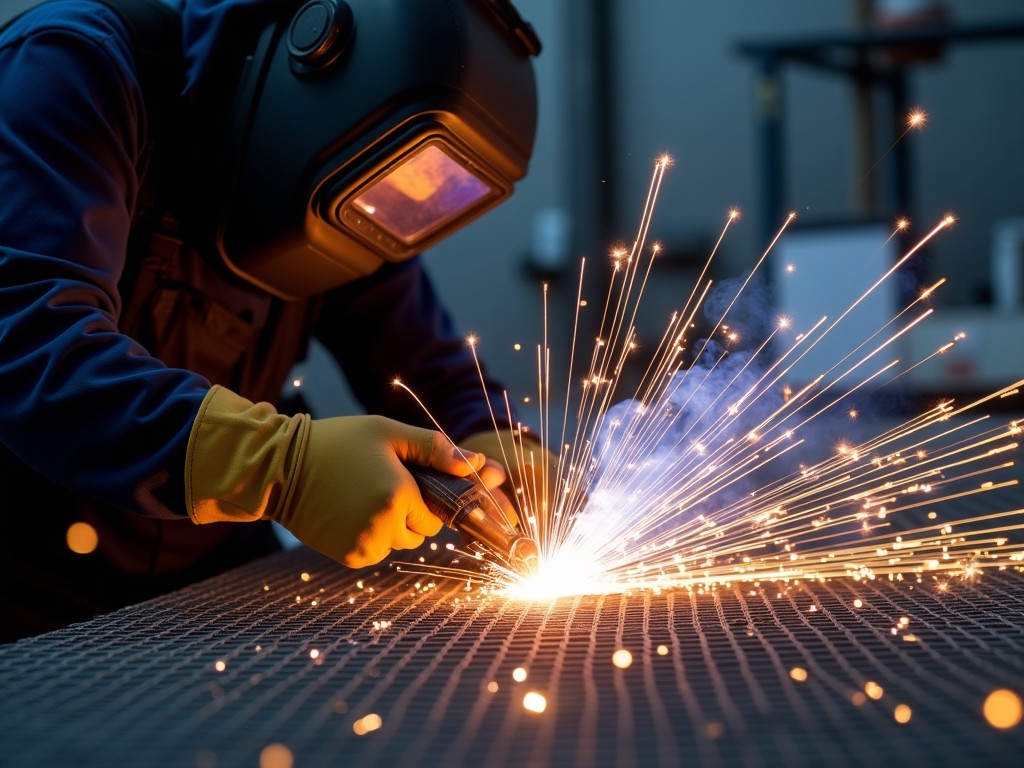
Welding Stainless Steel with Regular MIG Wire: Technical Considerations and Limitations
Industrial buyers evaluating welding processes for stainless steel components often question whether standard carbon steel MIG wire (such as ER70S-6) can be used effectively. This page explains the metallurgical, mechanical, and practical implications of using regular MIG wire on stainless steel substrates, based on welding engineering principles and field experience. Understanding these factors helps reduce the risk of premature failure, corrosion, or costly rework in fabricated assemblies.
Metallurgical Incompatibility of Carbon Steel Filler on Stainless Steel
Regular MIG wire, typically ER70S-6, contains approximately 0.06–0.09% carbon and 0.8–1.2% manganese with minimal alloying elements. When deposited onto austenitic stainless steel (e.g., 304, 316), this filler metal does not match the base metal’s chromium-nickel composition. The resulting weld metal forms a martensitic or ferritic microstructure instead of the austenitic structure required for corrosion resistance and ductility in stainless steel applications.
This mismatch leads to several detrimental effects: reduced corrosion resistance due to chromium depletion at the weld interface, increased susceptibility to cracking from thermal expansion mismatch, and diminished mechanical properties such as tensile strength and elongation. The weld bead may appear sound visually but lacks the alloy content necessary to maintain the passive oxide layer that protects stainless steel in corrosive environments.
Mechanical and Corrosion Performance Degradation
Welds made with ER70S-6 on 304 or 316 stainless steel typically exhibit tensile strengths 20–30% lower than those made with matching stainless filler (e.g., ER308L, ER316L). More critically, the heat-affected zone (HAZ) and weld metal become prone to intergranular corrosion and stress corrosion cracking in chloride-containing environments, such as marine settings or chemical processing plants.
Ferrite content in the weld metal increases significantly when carbon steel filler is used, which alters magnetic properties and can interfere with non-destructive testing methods like dye penetrant or ultrasonic inspection. In food-grade, pharmaceutical, or sanitary applications, such welds may harbor contaminants in micro-crevices formed during corrosion, violating hygiene standards.
When Temporary or Non-Critical Use May Be Considered
In non-structural, indoor, dry environments where corrosion exposure is negligible and mechanical loads are minimal—such as temporary fixtures, jigs, or shop-built prototypes—some fabricators may use ER70S-6 on stainless steel as a short-term expedient. However, even in these cases, the weld should be inspected for cracking and avoided in load-bearing joints.
Any use of carbon steel filler on stainless steel must be documented as a deviation from design specifications, and the welded assembly should not be expected to maintain the original material’s corrosion resistance or service life. Post-weld treatments like passivation cannot restore the lost alloy content in the weld metal.
Recommended Filler Metals for Stainless Steel MIG Welding
For reliable, code-compliant welds on stainless steel, use filler metals specifically formulated to match the base metal’s alloy content. Common options include ER308L for 304/304L, ER309L for dissimilar joints (e.g., stainless to carbon steel), and ER316L for 316/316L in corrosive environments. These wires contain 18–20% chromium and 8–12% nickel, with low carbon (<0.03%) to prevent sensitization.
Shielding gas selection is equally important: typically 98% Ar/2% CO₂ or 90% He/7.5% Ar/2.5% CO₂ for spray transfer, or tri-mix gases (He/Ar/CO₂) for pulsed MIG welding to control heat input and bead shape. Using the correct filler and gas combination ensures weld metal with equivalent corrosion resistance, toughness, and ferrite number (typically 3–8 FN) as specified in AWS A5.9.
| Parameter | Regular MIG Wire (ER70S-6) | Stainless Steel MIG Wire (ER308L/ER316L) |
|---|---|---|
| Chromium Content | 0.1–0.3% | 18–20% |
| Nickel Content | 0.1–0.5% | 8–12% |
| Carbon Content | 0.06–0.09% | ≤0.03% |
| Typical Tensile Strength (MPa) | 400–450 (on stainless) | 520–620 |
| Corrosion Resistance in NaCl | Poor (rapid pitting) | Good to excellent |
| Ferrite Number (FN) | >20 (undesirable) | 3–8 (acceptable) |
Risk Mitigation and Quality Assurance Practices
To prevent accidental use of incorrect filler metal, implement strict wire segregation and labeling procedures in the welding area. Use color-coded spools, dedicated wire feeders, and procedure qualification records (PQR) that specify the exact AWS classification (e.g., ER308LSi) for each stainless steel grade. Train welders to verify wire type before starting any joint on corrosion-resistant alloys.
For critical applications, require positive material identification (PMI) of the weld metal via XRF spectroscopy to confirm alloy content. Document all welding procedures in accordance with ASME Section IX or ISO 15614-1, and perform non-destructive testing (e.g., liquid penetrant or radiographic) on welds in pressure-retaining or safety-critical components.
Conclusion: Matching Filler Metal Is Non-Negotiable for Performance
Using regular MIG wire on stainless steel compromises the fundamental properties that justify the material’s selection—corrosion resistance, ductility, and high-temperature strength. While the process may appear successful initially, long-term performance in service environments will likely degrade, leading to leaks, structural weakness, or contamination risks.
Industrial buyers should specify matching stainless steel filler metals (ER308L, ER309L, ER316L) and qualified welding procedures to ensure weld integrity. Short-term convenience from using ER70S-6 is outweighed by the risk of failure, rework, or liability. Investing in correct consumables and procedures reduces uncertainty and supports reliable, code-compliant fabrication.
For technical consultation on welding procedure selection, filler metal compatibility, or qualification support for stainless steel fabrication, contact our engineering team.
Request Technical Support
More Products
Send Inquiry
If you are interested in our products, leave your information here and we will be in touch shortly.